GY Machining — High speed, high precision.
Precision CNC Machining Services for Prototypes & Production
CNC turned and milled components for prototypes, low-volume production and repeat orders.
STEP, STP, IGES, PDF, DWG and ZIP accepted
Capabilities
Precision CNC Machining Capabilities
GY provides high-quality CNC machined parts that meet your specifications and exceed your expectations. As an experienced CNC machining manufacturer, we make custom metal machined parts in aluminium, brass, stainless steel, copper, steel and more. Our capabilities also include CNC plastic machining in materials such as Delrin (POM), Nylon and PEEK. Our engineering and production staff provide CNC machining services to clients worldwide from our facility in Dongguan City, supported by a company-wide commitment to quality and customer satisfaction.
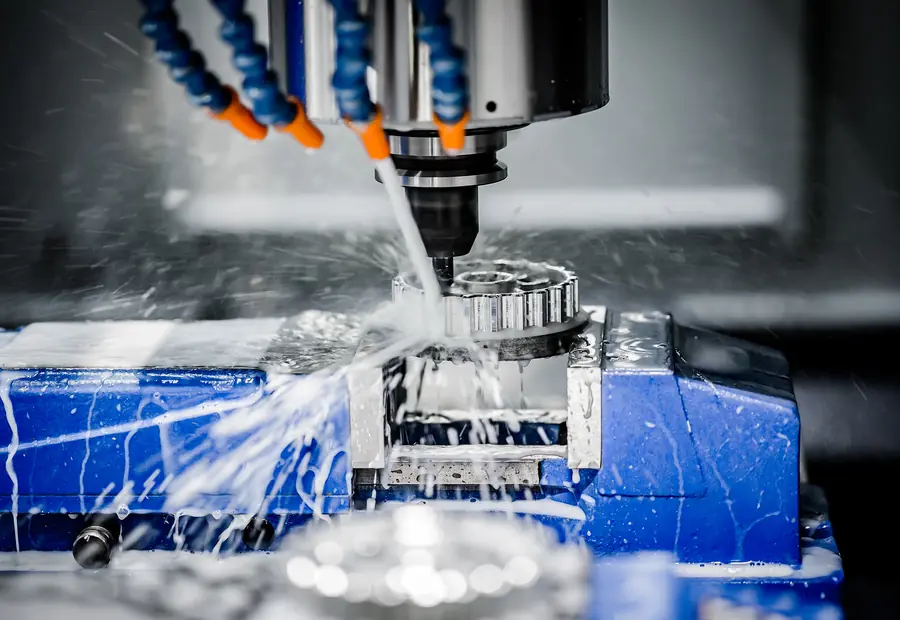
Milling
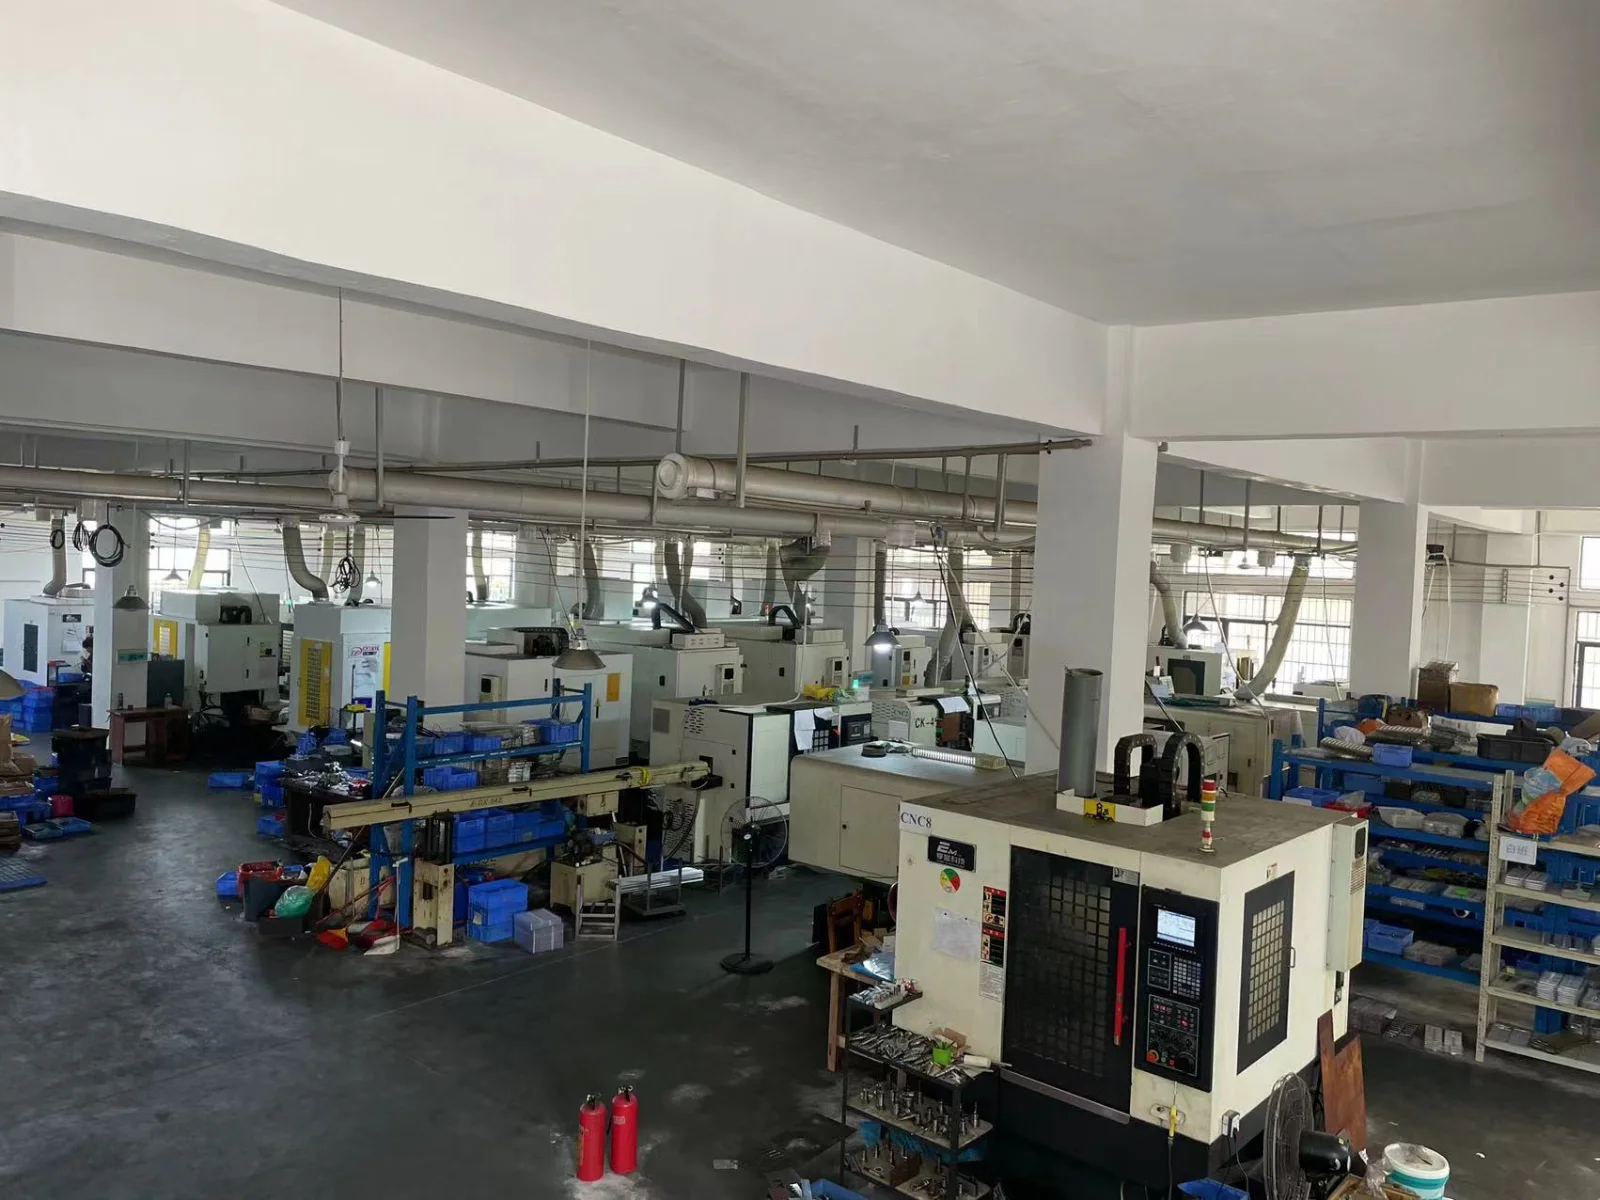
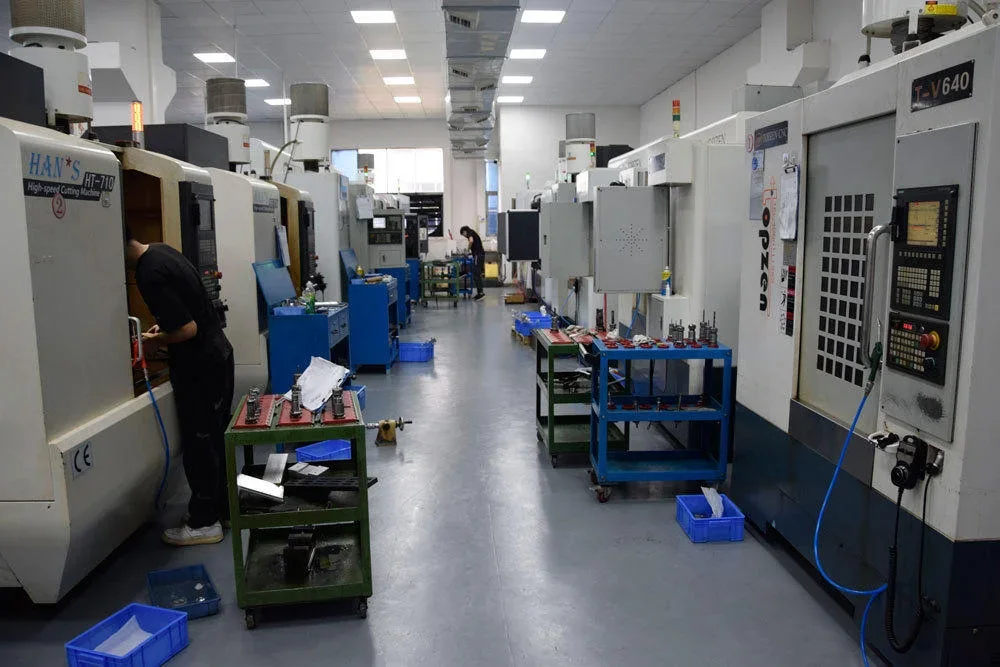
32 machining centres — 13 four-axis, 13 three-axis, 6 two-axis. This is where most toleranced work happens: bores, fits, seal faces, flatness.
- ±0.002 mm achievable on milled features
- Unmarked dimensions to DIN ISO 2768-m
- Part envelope up to roughly 800 × 600 × 500 mm
- Aluminium, stainless, tool steel, titanium, brass, engineering plastics
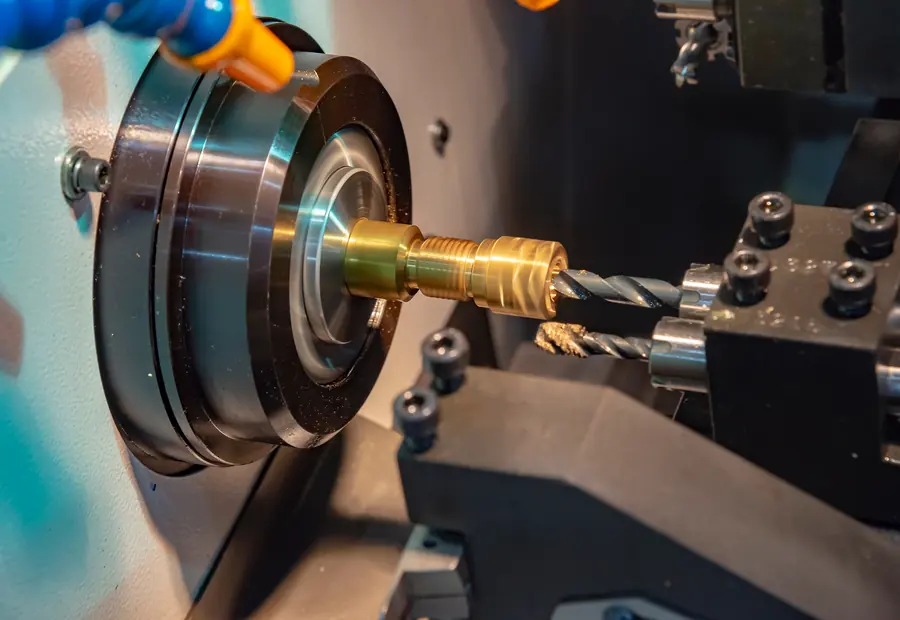
Turning
Eight CNC lathes for shafts, pins, bushings, adapters and sealing features, with second operations on the mill when the part needs them.
- Turned diameters from 3 mm to 250 mm
- Threads cut, not formed, where the drawing calls for it
- Concentricity checked against the drawing datum
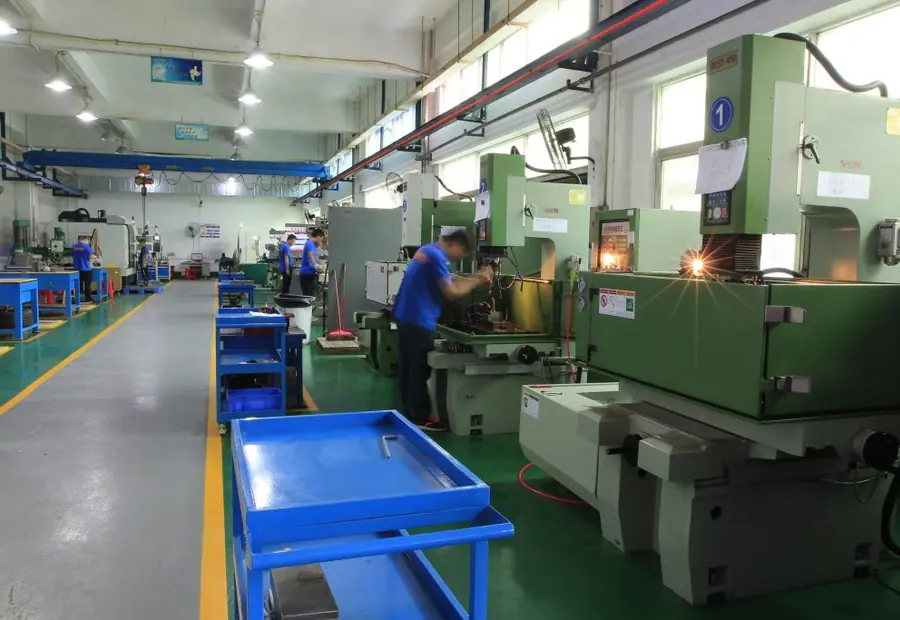
Wire EDM
Six wire EDM machines for shapes a cutter cannot produce — sharp internal corners, thin webs, and material already through heat treatment.
- Sharp internal corners with no corner radius
- Hardened steel cut after heat treatment
- Profiles taken straight from DXF or STEP
Sinker EDM
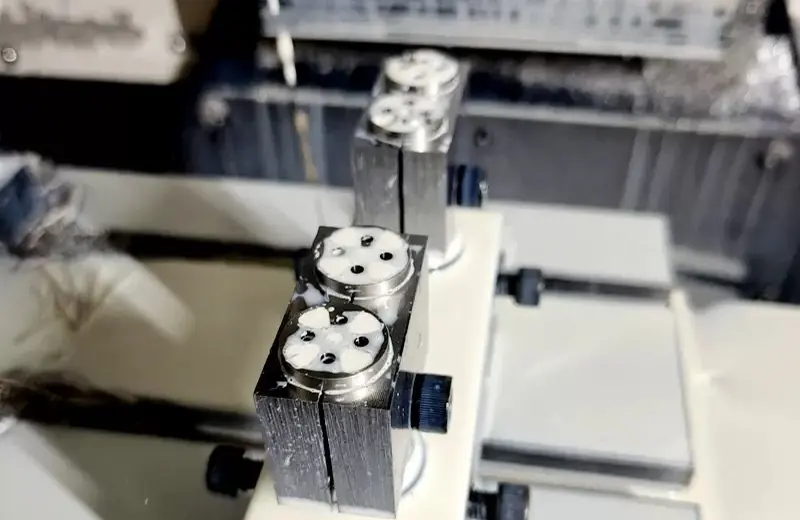
Six sinker EDM machines for blind pockets, keyways and cavities with no tool access. Electrodes are made here, on our own machines.
- Blind features and square-bottomed pockets
- Electrodes made in-house, on our own machines
- Used mainly on hardened tool steel
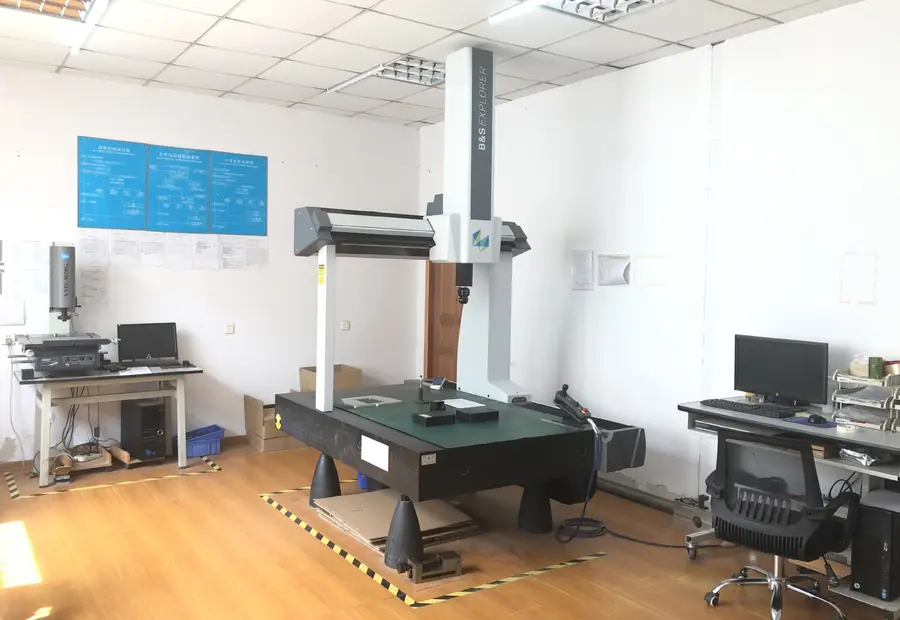
Measuring room
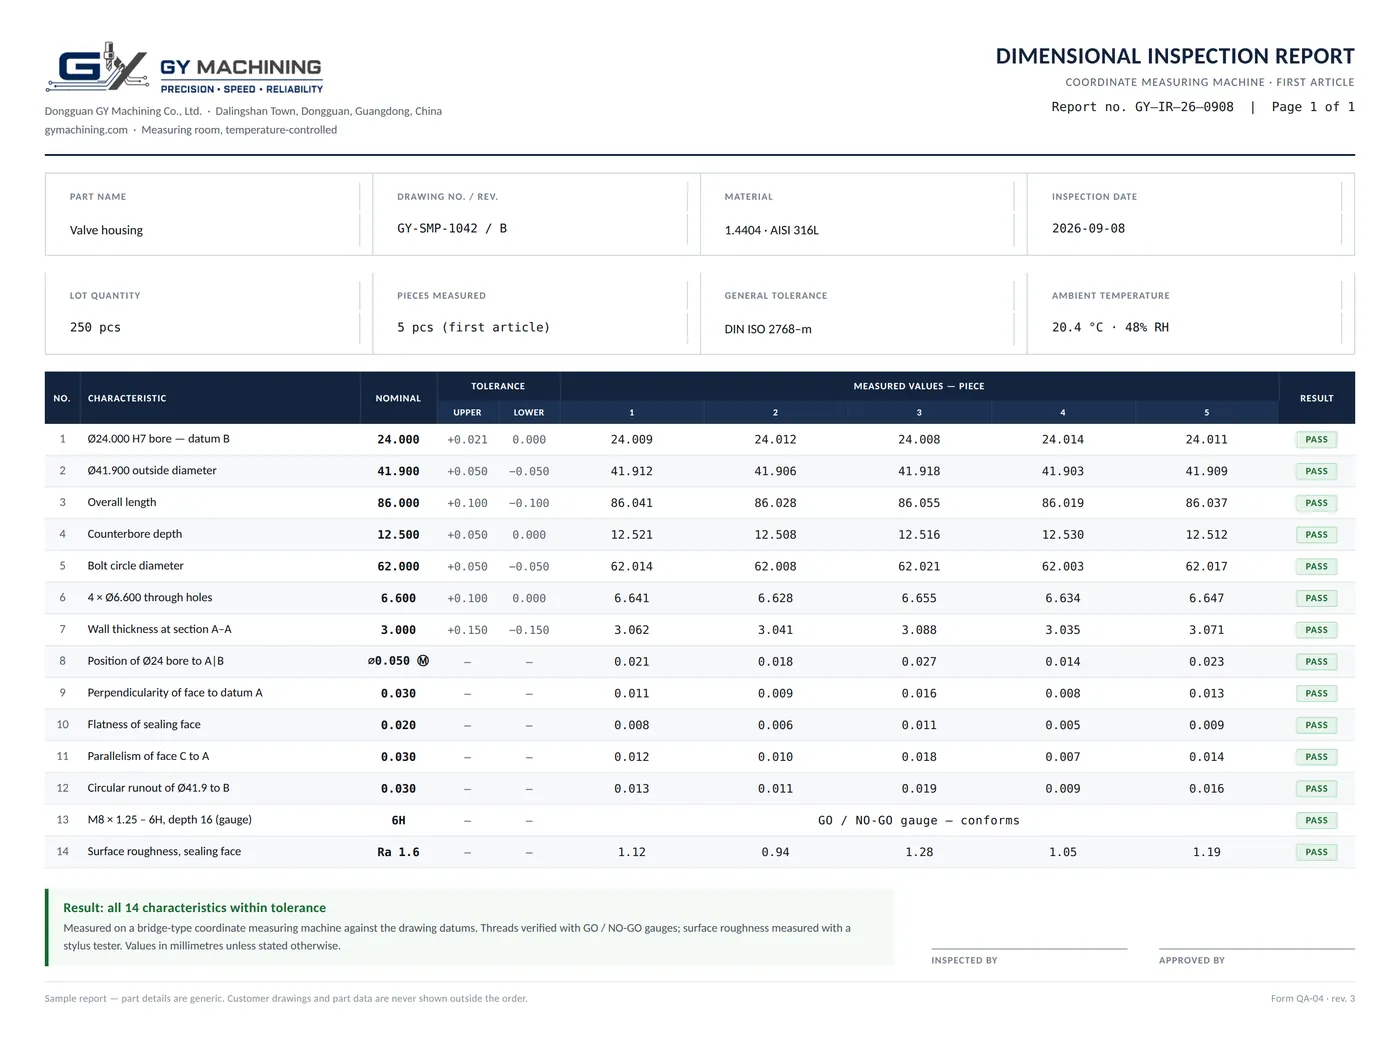
A coordinate measuring machine with a Renishaw PH10M probe head. Every production run starts here: the first part off the machine is measured before the rest is cut.
- First-article inspection before the run continues
- Report gives actual, nominal, upper and lower tolerance and deviation per feature
- Delivered as a PDF — ask for it with the order
- If a toleranced feature is out, you get a phone call, not a box of scrap
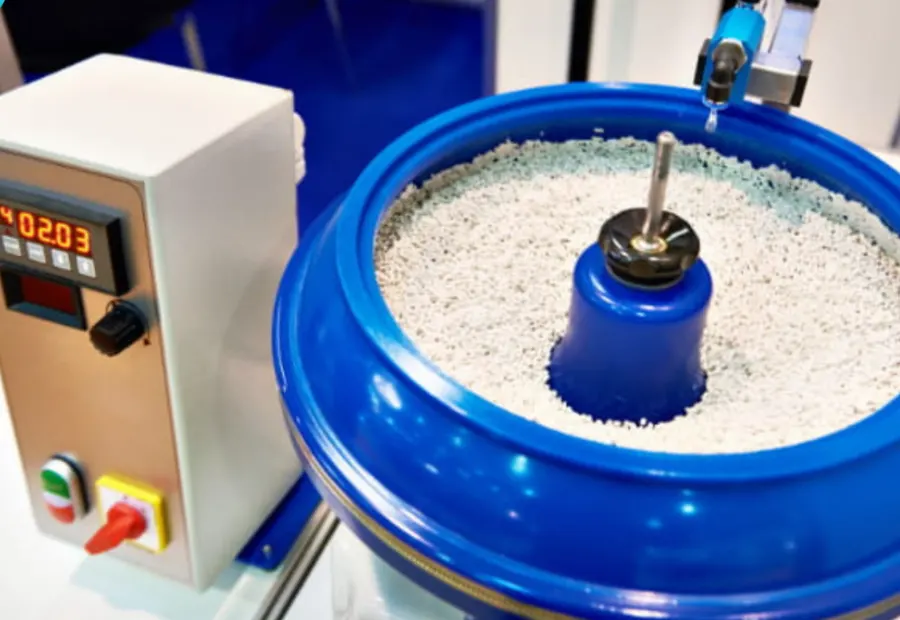
Finishing
Tumbling and deburring happen on our own two machines. Anodising, black oxide, plating, blasting, polishing and powder coating run at shops we work with — we organise it, and we tell you so you know where the part goes.
- Tumbling (stone-wash) in-house, two machines
- Anodising, plating, blasting, coating coordinated outside
- One supplier, one invoice, one delivery
What we hold
The features people actually buy from us
Toleranced work is most of what runs here. These are the things that usually decide whether a part is accepted or sent back.
Fits and bores
Mark the fit on the drawing and it is measured on the CMM against that fit, not eyeballed with a caliper.
Seal faces and flatness
Faces that have to seal get measured for flatness against the drawing datum before the run continues.
Concentricity and runout
Turned and milled features on the same part are checked against the datum the drawing specifies.
Threads
Cut rather than formed where the drawing requires it, so the thread form matches what you specified.
Sharp internal corners
Where a cutter would leave a radius, the corner is cut on wire EDM instead.
Hardened material
Tool steel is machined after heat treatment on wire and sinker EDM, so the tolerance survives hardening.
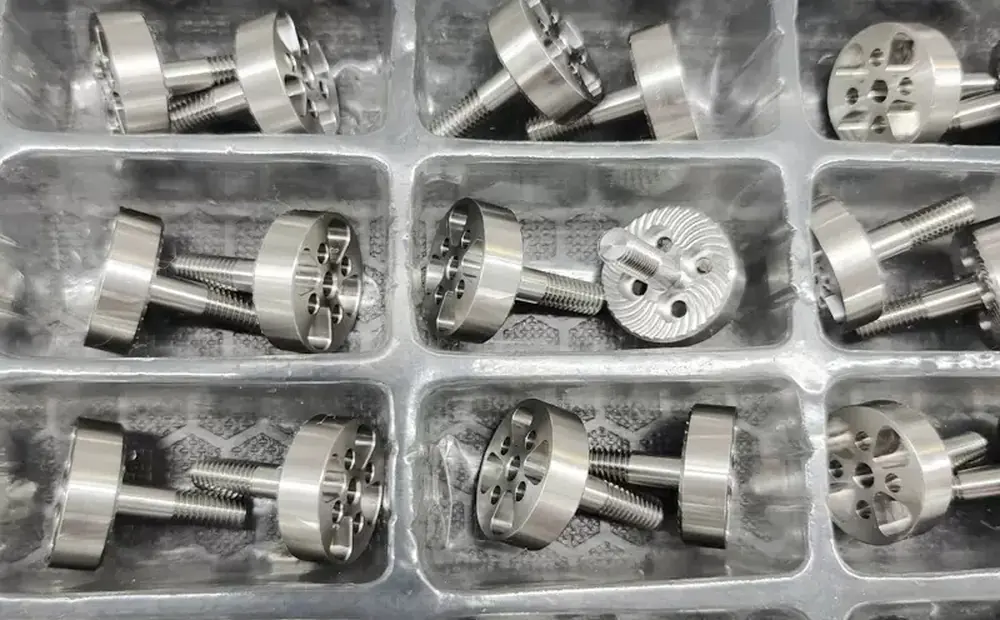
Why choose GY for CNC machining?
Accurate machining
±0.01 mm typical on toleranced features, ±0.002 mm achievable on milled features — every first article measured on the CMM.
Milling, turning, wire and sinker EDM
32 machining centres, 8 lathes and 12 EDM machines under one roof. 2-, 3- and 4-axis — no 5-axis, and we say so up front.
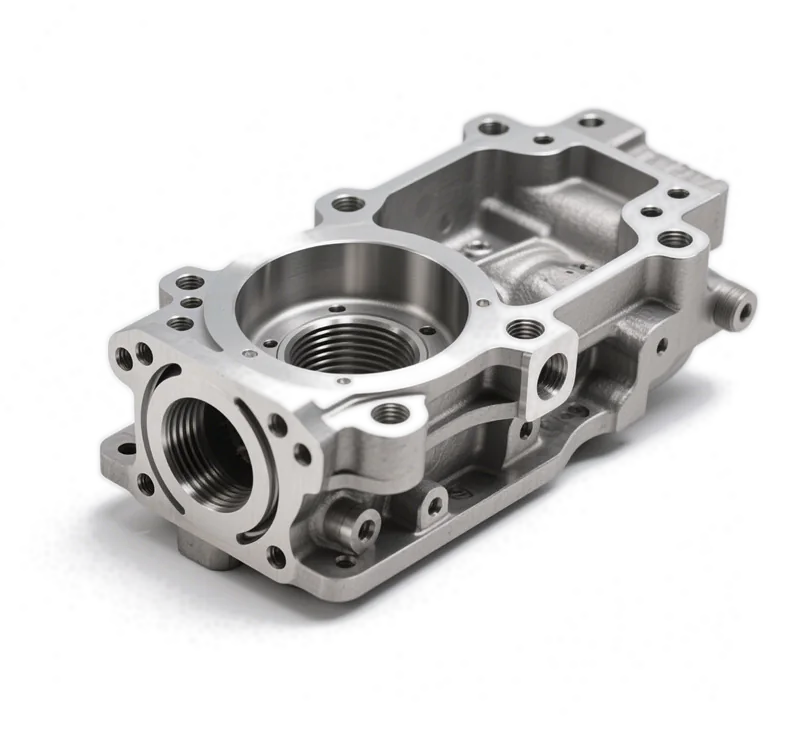
Finishes to match the drawing
As-machined, bead blasted, anodised, black oxide, powder coated or plated. Tumbling in-house, the rest through partner shops.
Fast turnarounds
Quote within 16 hours, lead time stated on the quote. Parts ship by DHL, FedEx or UPS, or to your forwarder in Shenzhen.
Recent work
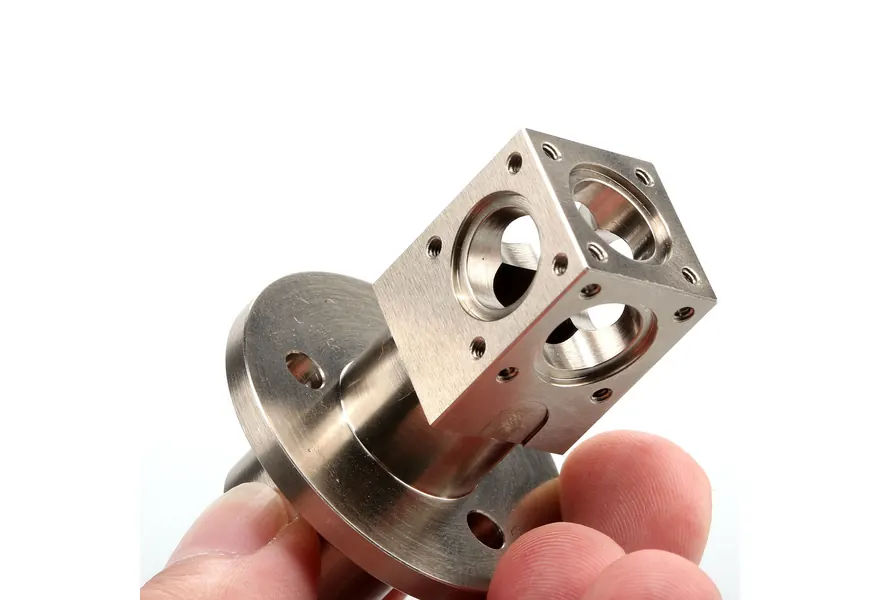
Parts we machine
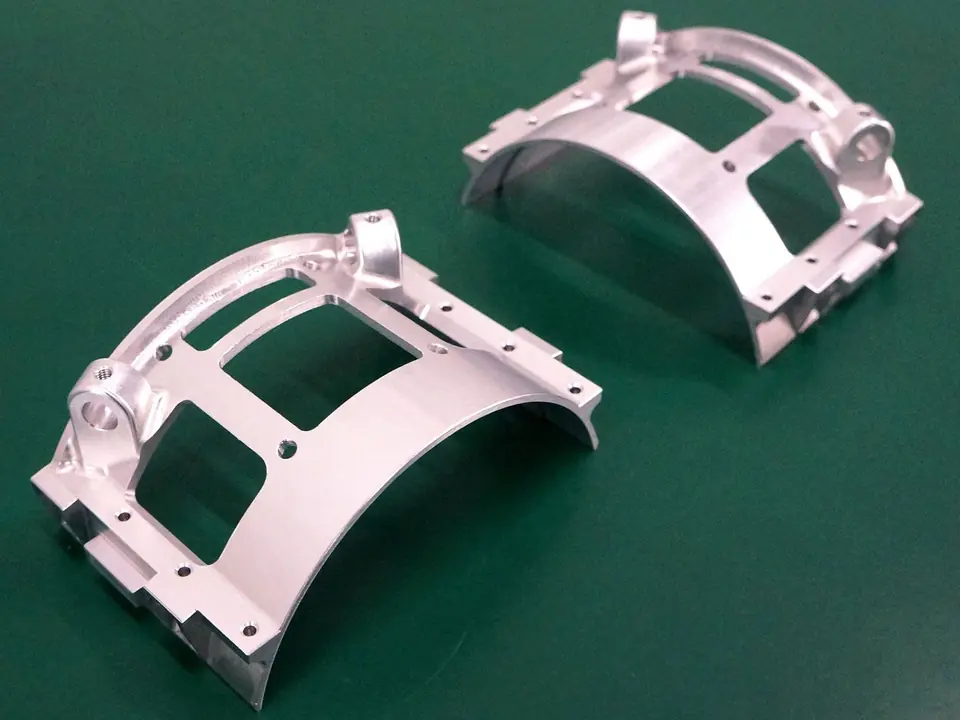
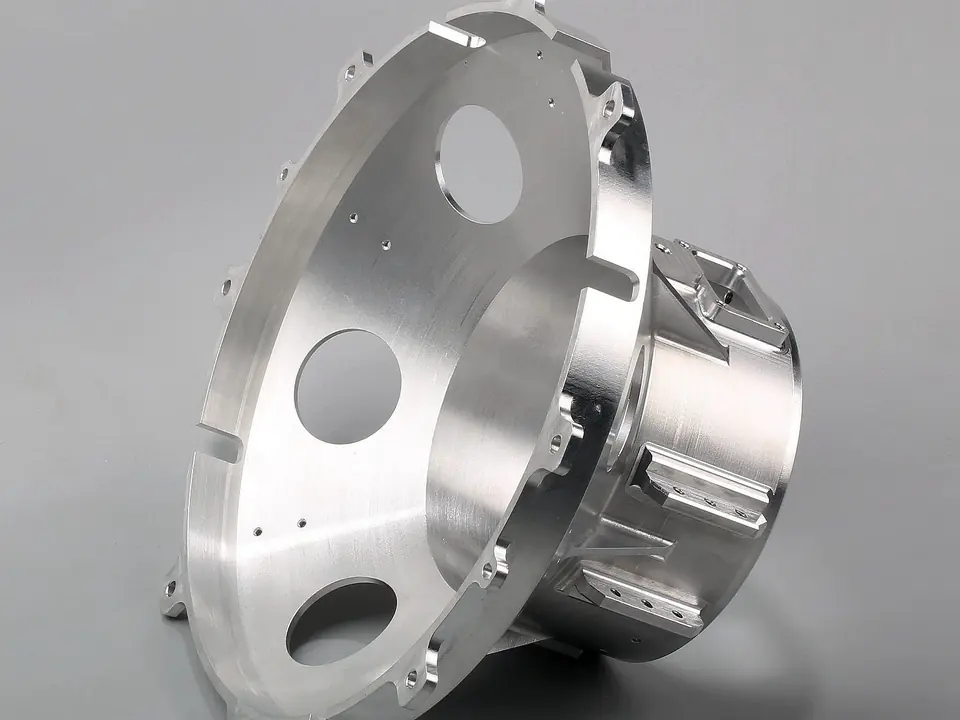
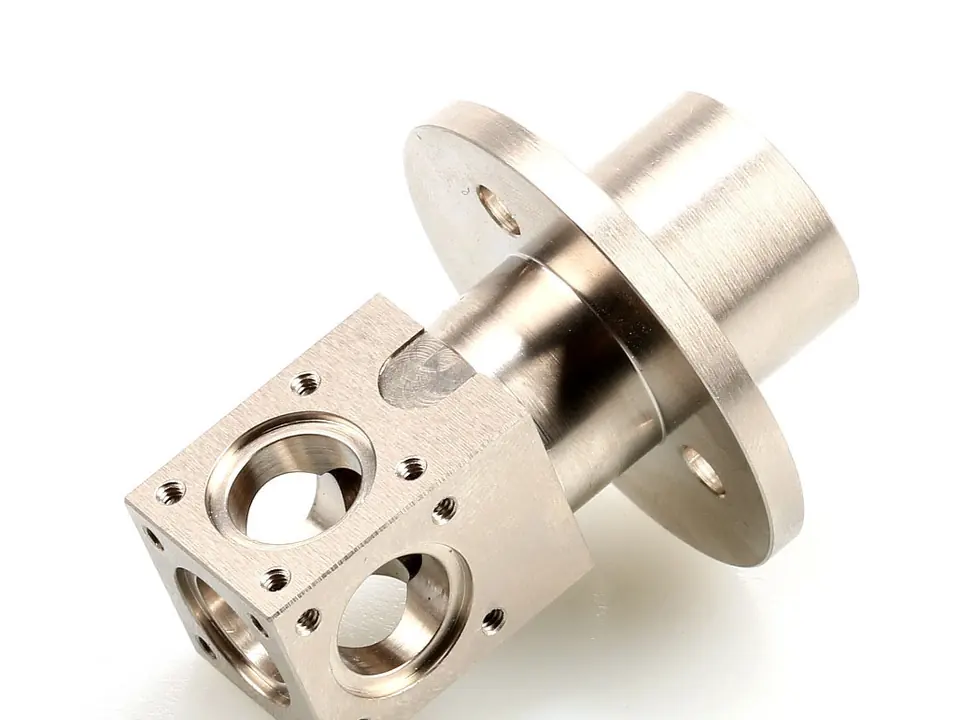
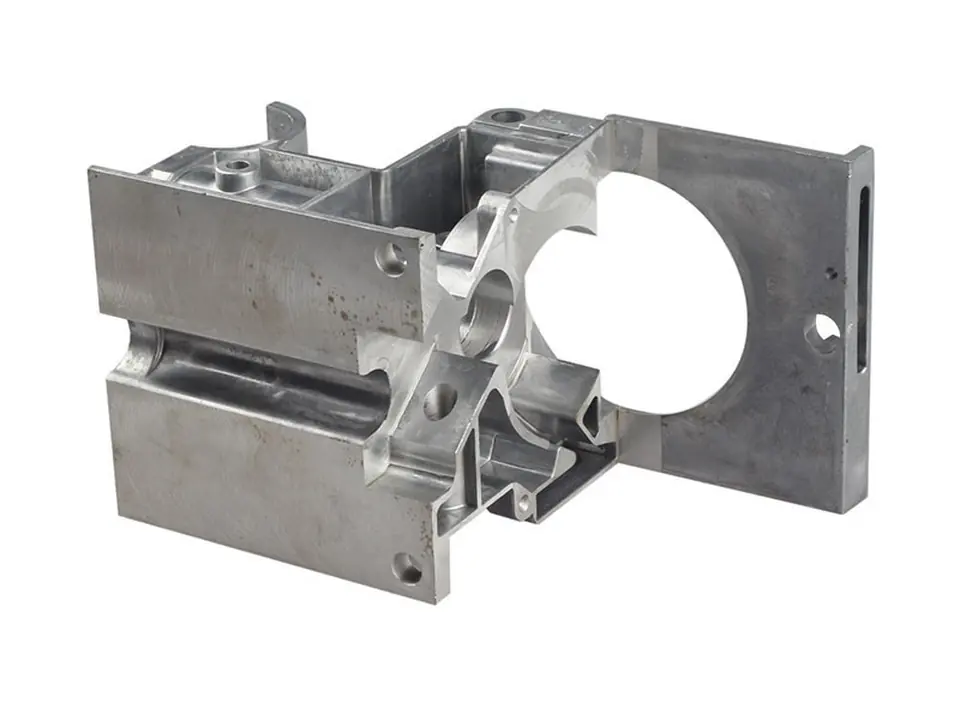
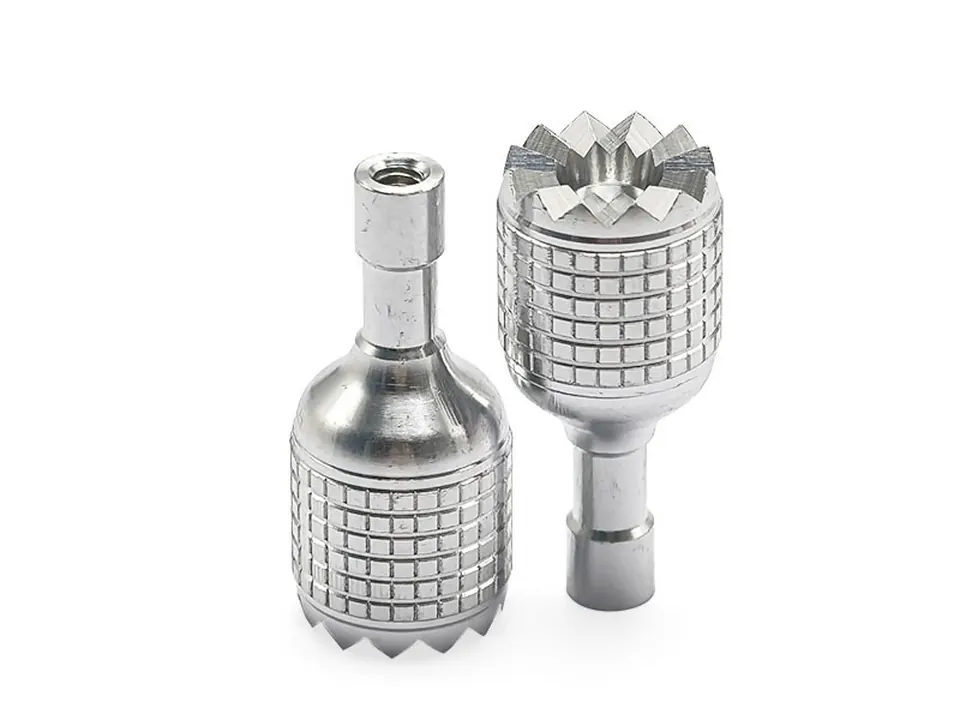
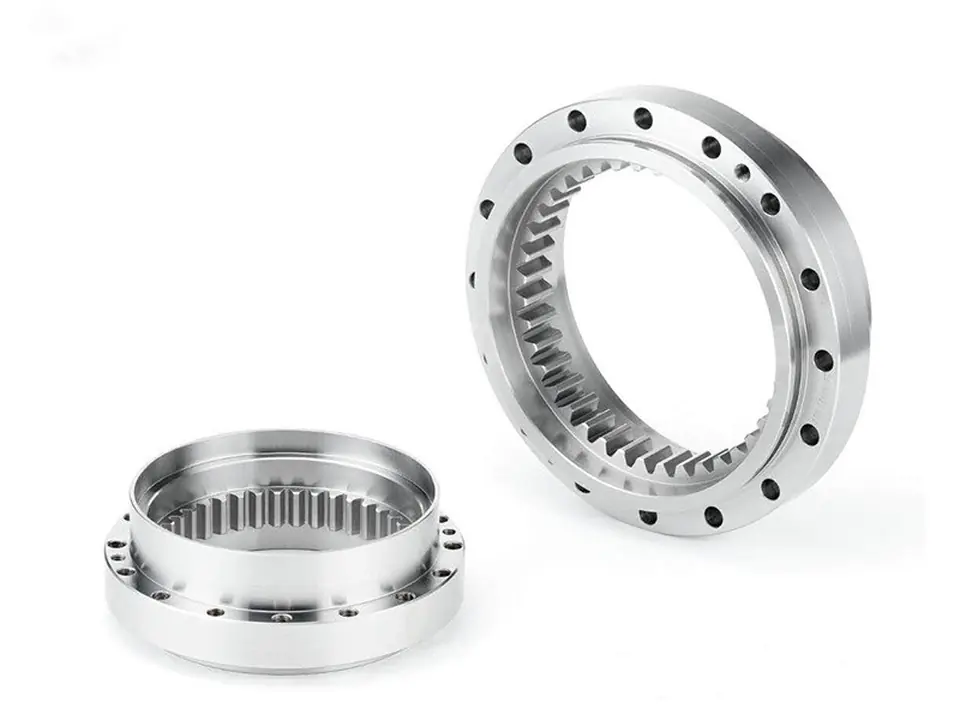
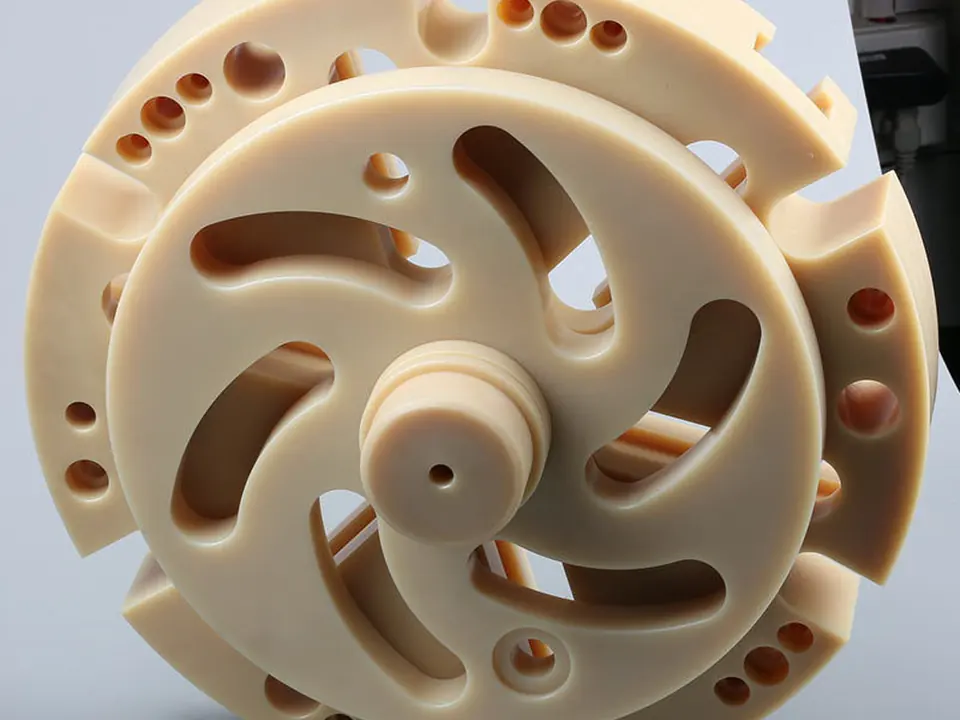
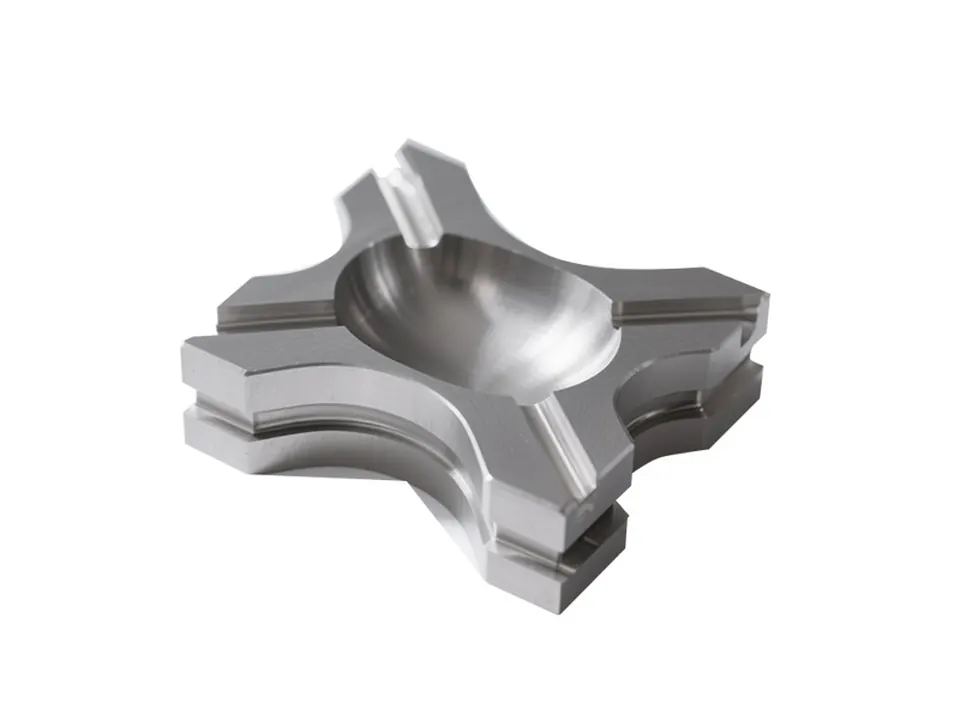
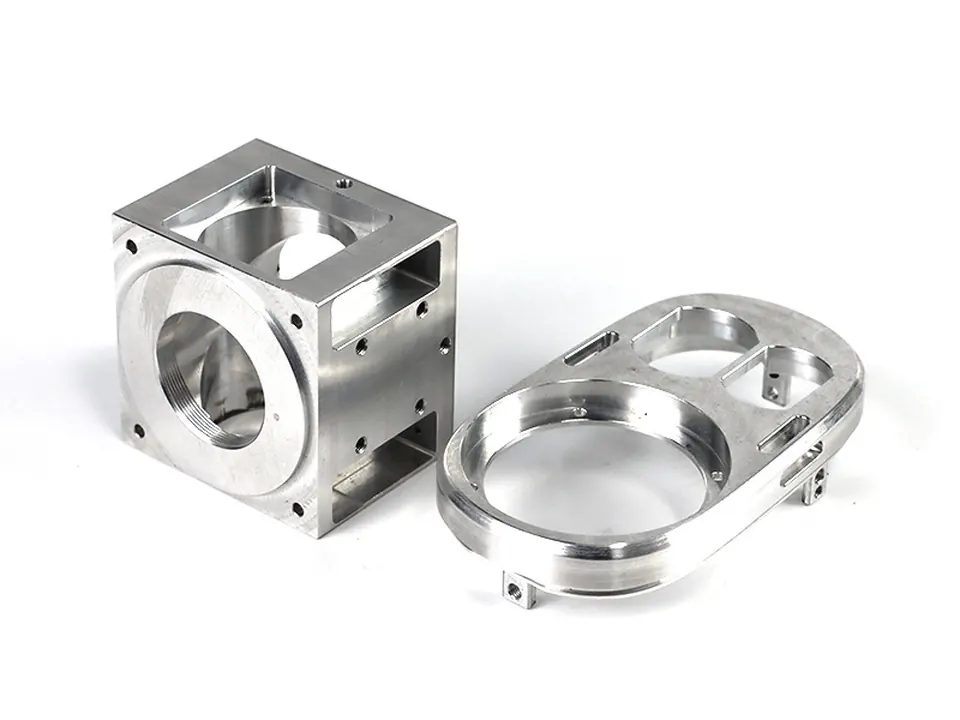
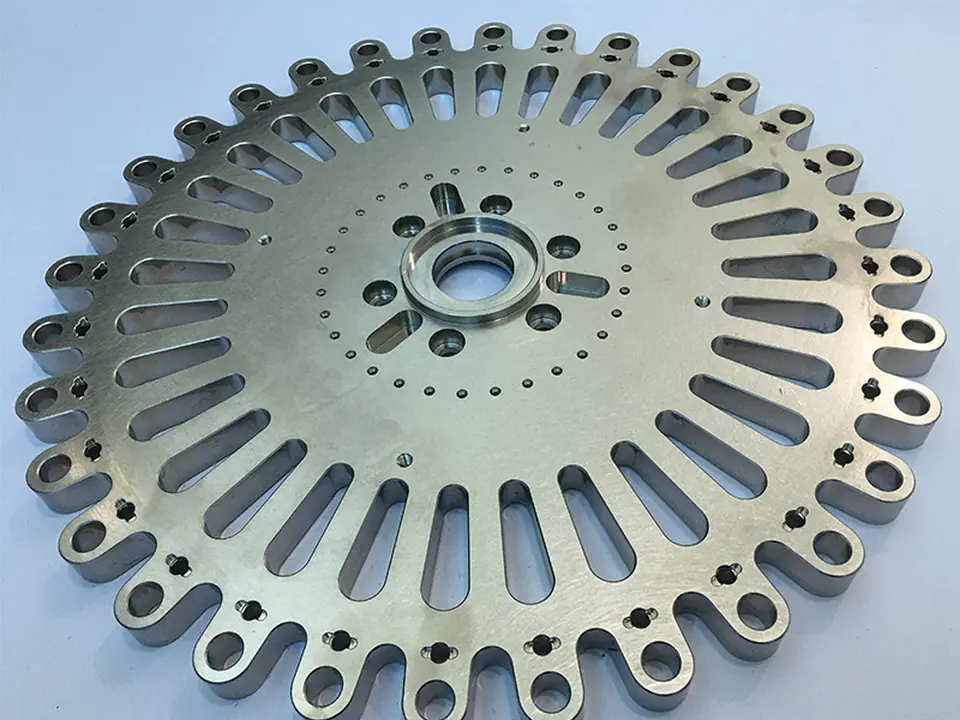
Our shop
Professional CNC Machining Services for Custom Precision Parts
GY provides custom CNC machining services for rapid prototyping, batch production and complex parts. Our advanced CNC machining capabilities are trusted by engineers and industrial designers, from innovative start-ups to Fortune 500 companies, across the automotive, aerospace, medical and robotics industries.
Tolerance standards we work to
- ✓ISO 2768-m by default; ISO 2768-f on request
- ✓ISO 286 fits — IT8, IT7, IT6, gauged or measured on the CMM
- ✓Tighter tolerances — mark the drawing, we quote to it
- ✓EN 10204 3.1 material certificates on request
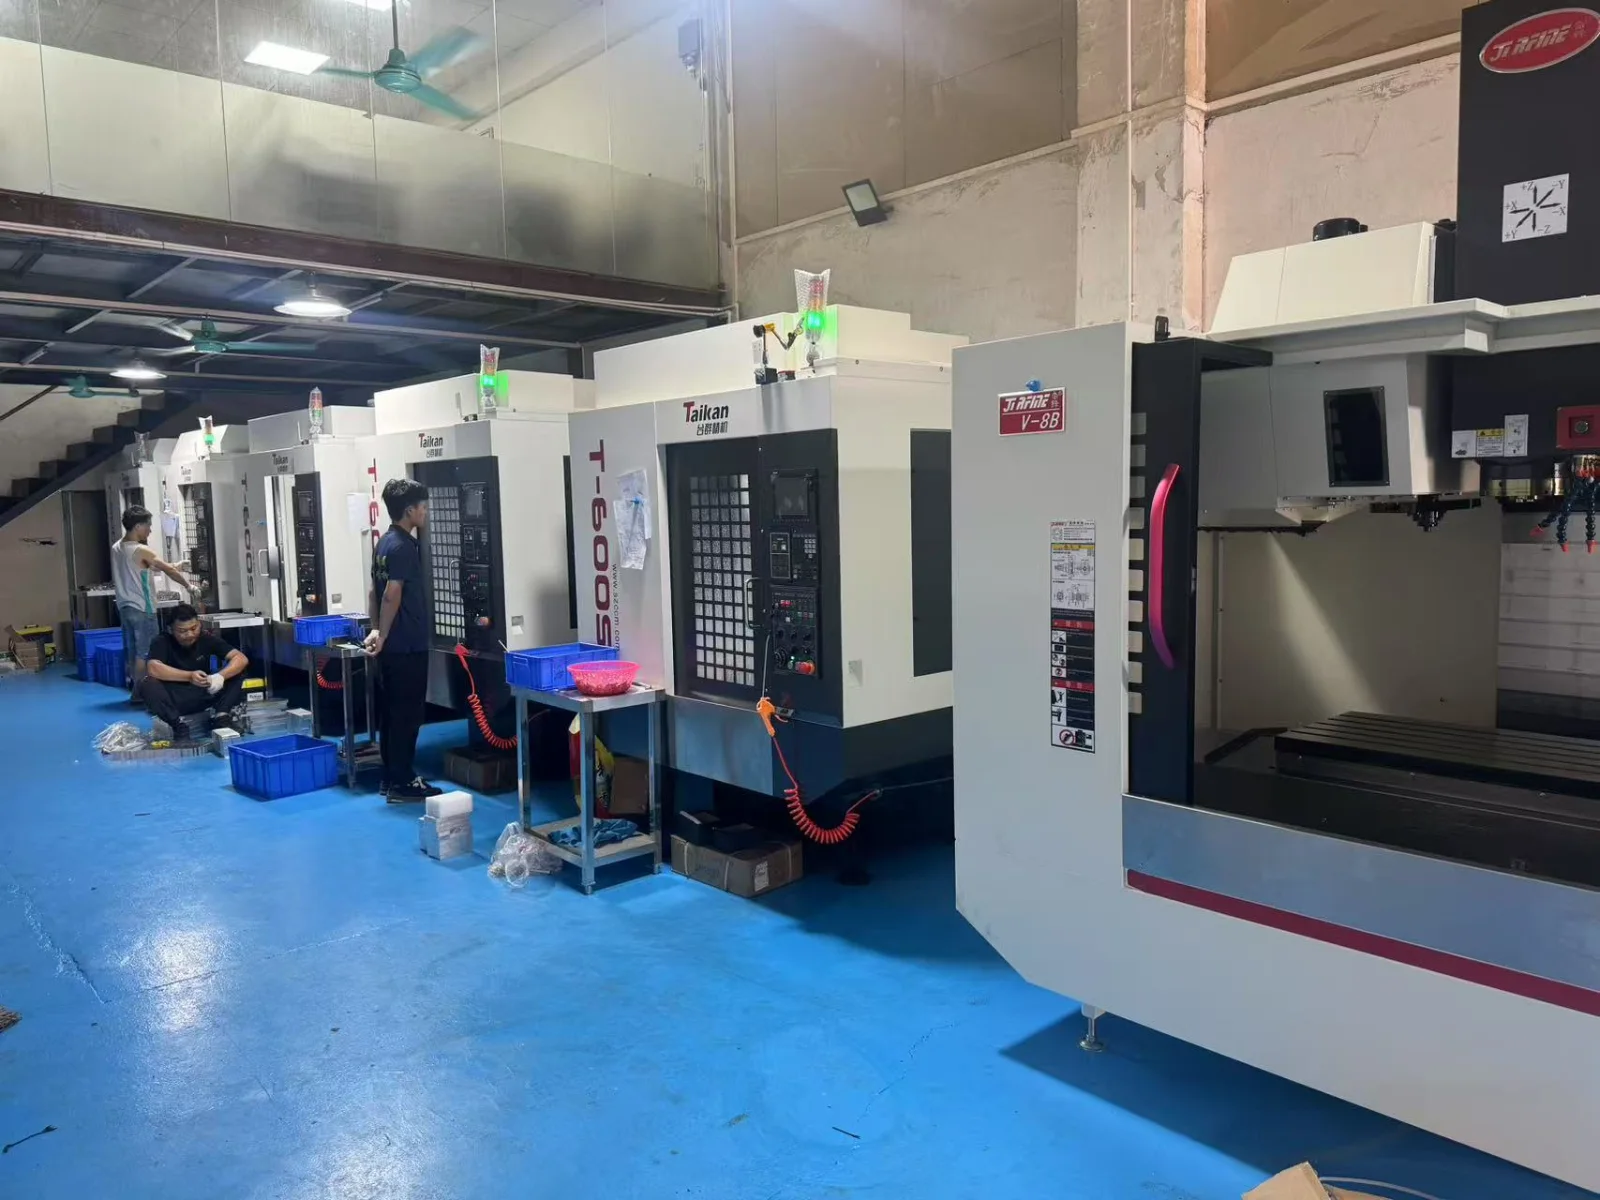
| Qty | Machine |
|---|---|
| 32 | CNC machining centres — 13 × 4-axis, 13 × 3-axis, 6 × 2-axis |
| 8 | CNC lathes |
| 6 | Wire EDM (WEDM) |
| 6 | Sinker EDM |
| 4 | Punching machines, plus forming and welding |
| 2 | Tumbling machines (stone-wash) |
| 4 | Engineers on staff |
Materials & finishes
Common CNC Materials & Surface Finishes
Not sure which material or finish best suits your project? We can recommend practical options based on application, tolerance, cost and lead time.
Common Metal Materials
- Aluminium 6061 / 7075
- Lightweight, machinable and versatile
- Stainless Steel 303 / 304 / 316
- Corrosion-resistant and durable
- Tool Steel / Carbon Steel
- High strength and wear resistance
- Brass / Copper
- Suitable for electrical components and decorative parts
- Titanium
- High strength-to-weight ratio and corrosion resistance
Common Plastic Materials
- ABS / PC / Acrylic
- For prototypes and enclosures
- POM (Delrin) / Nylon
- For moving and wear-resistant parts
- PTFE / UHMW
- For low-friction applications
- PEEK / PPS
- For high-temperature and high-performance applications
- PVC / PP
- For cost-sensitive functional parts
Surface Finishes
- As-Machined / Brushing
- Basic production finishes
- Bead Blasting / Polishing
- Better surface consistency
- Anodising / Black Oxide
- Protection and visual enhancement
- Powder Coating / Painting
- For higher performance requirements
- Laser Marking / Silk Screening
- Part identification and branding
Material designations we work to
| Material no. | Designation | Also known as |
|---|---|---|
| 3.3211 | EN AW-6061 · AlMg1SiCu | AA 6061 |
| 3.2315 | EN AW-6082 · AlSi1MgMn | AA 6082 |
| 3.4365 | EN AW-7075 · AlZn5,5MgCu | AA 7075 |
| 3.3547 | EN AW-5083 · AlMg4,5Mn0,7 | AA 5083 |
| 1.4301 | X5CrNi18-10 | AISI 304 |
| 1.4404 | X2CrNiMo17-12-2 | AISI 316L |
| 1.0038 | S235JR | St 37-2 |
| 1.0570 | S355J2 | St 52-3 |
| 1.7225 | 42CrMo4 | AISI 4140 |
| 1.2379 | X153CrMoV12 | AISI D2 |
| 2.0401 | CuZn39Pb3 | Ms58 |
| 2.0065 | Cu-ETP | C11000 |
| 3.7035 | Ti Grade 2 | R50400 |
| 3.7165 | TiAl6V4 | Ti Grade 5 |
Materials and advice
From prototyping to production, we offer extensive material options and expert advice to help guide you through every stage of the production process.
Engineering plastics in stock or sourced
Inspection & documents
What we measure, what you get on paper, and what we cannot give you
Read the right-hand column before you order. We would rather lose the enquiry than the order.
✓What you get
- Achievable milling accuracy ±0.002 mm
- on milled features — not on every feature of every part. Mark the tight ones on the drawing; without a mark we work to DIN ISO 2768-m.
- First-article inspection, every production run
- The first part is measured on the coordinate measuring machine before the rest of the run is cut. This is not an extra you order; it is how we work.
- Dimensional report
- Actual value, nominal, upper and lower tolerance and the deviation for each measured feature, tied to the part and the measuring programme it came from. PDF. Ask for it with the order — it does not happen automatically.
- EN 10204 3.1 material certificate
- on request, with batch / heat number, ordered against the certificate and passed through with the parts. Certified stock has a longer lead time, so say so with the enquiry.
- An engineer's opinion before you commit
- If a tolerance is tighter than the function needs, we say so. Loosening one dimension often costs less than the whole rest of the part.
- Drawing and data confidentiality
- Your files go to nobody outside the shop. NDA on request, before you send anything.
!What we do not have
- No ISO 9001 certificate
- We are not currently certified. No certificate does not mean unprofessional — it means you judge us by the part and the report, not by the binder. If your supplier approval requires the certificate, we would rather tell you now than after the order.
- No EMPB to VDA Volume 2, no PPAP
- We do not produce formal first-article reports in the automotive formats. A normal dimensional report you can have; those two you cannot.
- No 5-axis simultaneous machining
- Our centres are 2-, 3- and 4-axis. A part that genuinely needs simultaneous 5-axis work is not for us, and we will say so when we see the drawing rather than find out on the machine.
Process
From Upload to Delivery
Turn your CAD files into finished parts through a clear, four-step process.
Upload Your Design
Upload your CAD files and drawings, along with material, quantity and finishing requirements.
Quote & DFM Review
Pricing and lead time within 16 hours, with DFM feedback where the drawing needs it.
CNC Production
Your parts are machined in-house, with a first article measured before the run continues.
Inspection & Shipping
Final inspection, quality documents on request, and shipping by DHL, FedEx or UPS.
Your drawings stay inside the shop. NDA on request.
- No minimum order quantity
- Engineering review before every quote
- First article measured on the CMM
Send the drawing. We will tell you what we can hold.
Price, lead time, and an engineer's opinion on the tolerances — usually back within 16 hours.
FAQ
Questions we get asked
How tight a tolerance can you really hold?
What exactly is in the dimensional report?
Is the first article measured on every job?
Are you ISO 9001 certified?
Do you machine hardened material?
What is the minimum order?
Who actually makes the parts?
Will you sign an NDA?
Contact
Talk to us
Send the drawing and the quantity. If something is unclear we ask rather than guess.
- eileen@gymachining.com
- Phone / WhatsApp
- +86 137 9012 4916
- Address
- 2nd Floor, Hongfu Building, No. 45 Lianma Road,
Dalingshan Town, Dongguan, Guangdong 523129, China - Hours
- Mon–Sat 08:00–23:00 Beijing time (GMT+8)
- Quote turnaround
- Within 16 hours